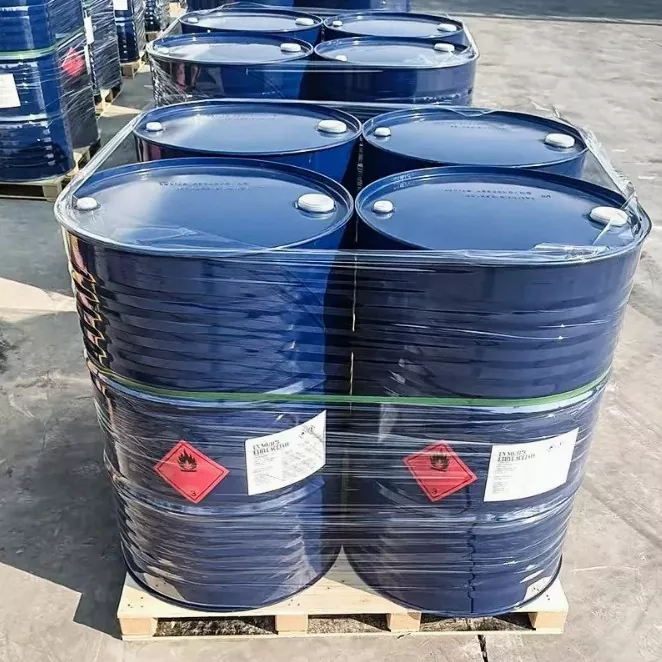
For food ingredient and flavor manufacturers, solvent selection is closely related to aroma quality, extraction efficiency, residual control, and consistency between production batches. AOLANSU supplies high-purity Food Grade Ethyl Acetate solutions for customers that require controlled chemical properties in flavor preparation, botanical extraction, beverage processing, and related food-industry applications.
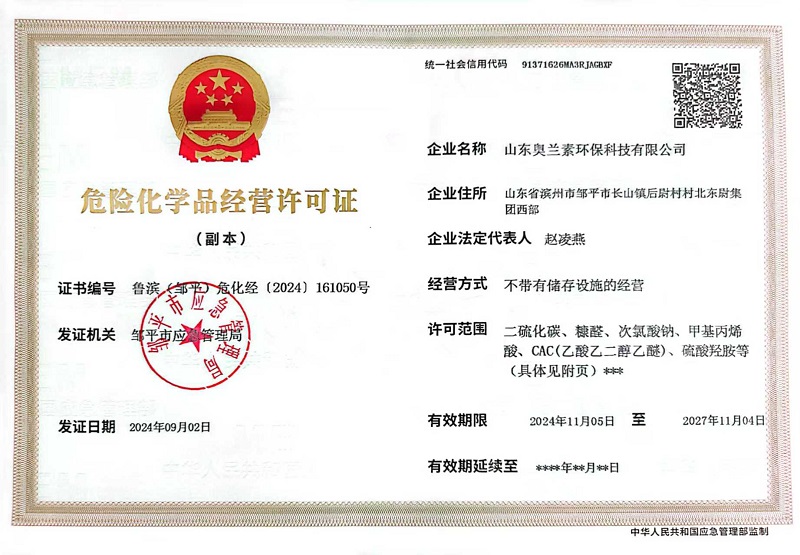
Shandong Aolansu Environmental Technology Co., Ltd., located in Binzhou, Shandong, China, specializes in high-purity chemical production and international supply. AOLANSU applies purification, laboratory testing, and batch management procedures to provide stable material quality. The company also holds a Hazardous Chemicals Business License for compliant chemical business operations.
Food-related solvent applications place particular emphasis on purity, moisture, acidity, evaporation residue, odor, and batch consistency. These factors can influence extraction performance and the sensory characteristics of flavor or natural ingredient products.
The product offers high solvency for selected aromatic and natural compounds while evaporating efficiently during controlled processing. Its characteristic fruity odor and controlled impurity profile make it suitable for applications where solvent characteristics need to be considered alongside the quality of the final ingredient.
A purity level of ≥99.5% is supported by routine quality testing. Moisture, acidity, evaporation residue, color, and trace impurities are also monitored to provide a more predictable raw material for food ingredient processing.
Controlling these parameters can help manufacturers reduce unwanted solvent-related odor, flavor interference, and variations during extraction or flavor preparation.
For flavor manufacturers, solvent quality cannot be evaluated only through chemical purity. Odor characteristics and residual behavior may also affect the processing of aroma compounds.
Controlled purification helps maintain consistent material characteristics between batches, giving flavor producers a more stable input when preparing fruit flavors, beverage essences, bakery flavors, and other aroma formulations.
The product combines strong dissolving capability with relatively rapid evaporation. This characteristic is useful in processes where the solvent needs to perform its extraction or carrier function and then be effectively removed under controlled processing conditions.
Manufacturers can therefore evaluate both extraction efficiency and downstream solvent-removal requirements when selecting the appropriate grade.
Food Grade Ethyl Acetate is widely used as an extraction and carrier solvent in flavor manufacturing. It can dissolve selected aroma compounds and natural flavor components for the preparation of fruit flavors, beverage flavors, bakery flavors, and other food aroma formulations.
Its evaporation characteristics can support subsequent processing while helping manufacturers maintain the intended sensory profile of the finished flavor system.
Botanical materials, herbs, spices, and other natural raw materials often contain compounds with different solubility characteristics. Ethyl acetate can be used as an extraction medium for selected compounds during natural ingredient processing.
Controlled purity and consistent solvent properties allow manufacturers to maintain more predictable extraction conditions across production batches.
In beverage ingredient production, solvent quality can influence the preparation and handling of concentrated flavor components. The product can be used in controlled flavor-processing procedures where high-purity solvent characteristics are required.
Manufacturers can select the appropriate specification according to their formulation process, finished-product requirements, and applicable food regulations.
Ethyl acetate is also used in coffee and tea processing, including certain decaffeination-related applications. Its solvent properties allow selected compounds to be extracted under controlled processing conditions.
For these applications, buyers should evaluate solvent specifications, process compatibility, regulatory requirements, and downstream residue-control procedures before commercial use.
AOLANSU uses multi-stage distillation and related purification procedures to improve solvent purity and remove unwanted components. Controlled purification helps maintain stable chemical characteristics suitable for demanding food and flavor processing applications.
Before shipment, batches undergo laboratory testing covering key quality parameters such as purity, moisture content, acidity, evaporation residue, and appearance.
This testing provides customers with measurable product information rather than relying solely on general grade descriptions.
Production and laboratory records are maintained for individual batches. Batch identification supports customer incoming inspection, internal quality management, and supply-chain traceability.
| Parameter | Specification | Test Method |
|---|---|---|
| Purity | ≥99.5% | Gas Chromatography (GC) |
| Moisture Content | ≤0.10% | Karl Fischer Method |
| Acidity (as CH₃COOH) | ≤0.005% | Titration |
| Heavy Metals | ≤10 ppm | ICP-MS |
| Arsenic Content | ≤1 ppm | ICP-MS |
| Evaporation Residue | ≤0.002% | Gravimetric Method |
| Color | ≤10 APHA | Visual Method |
| Relative Density | 0.894–0.898 | Hydrometer |
| Refractive Index | 1.371–1.376 | Refractometer |
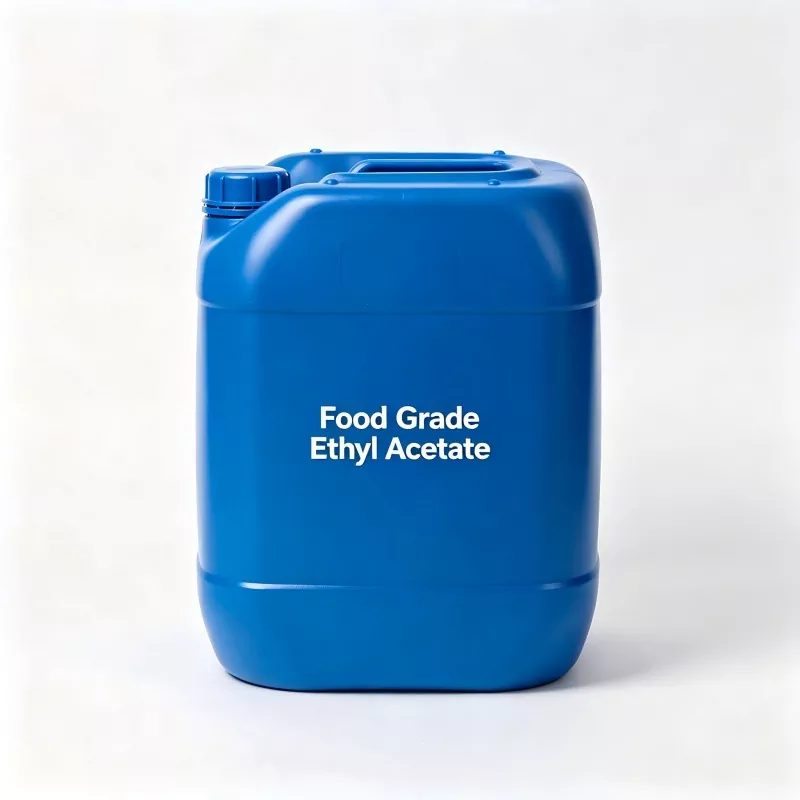
| Packaging | Food-Compatible HDPE Drums / IBC Containers / ISO Tank | - |
Specifications, food-use status, applicable regulatory requirements, and documentation should be confirmed according to the customer's intended application and destination market before procurement.
A Southeast Asian flavor manufacturer was looking for a stable Food Grade Ethyl Acetate supplier to improve consistency during flavor formulation processes. Previous solvent supply differences affected production stability and required additional incoming material checks.
After adopting AOLANSU Food Grade Ethyl Acetate, the customer achieved more consistent solvent performance during flavor preparation. Stable purity levels and complete COA documentation helped simplify quality verification procedures and improve raw material management efficiency.
Through continuous supply support and reliable product quality, AOLANSU established a long-term cooperation relationship with the customer.
Different food manufacturers, flavor companies, and ingredient processors have different requirements for solvent quality, delivery frequency, documentation, and supply volume. AOLANSU provides flexible supply solutions based on customer application needs, helping buyers select suitable product specifications and establish reliable long-term sourcing channels.
Flavor producers often require stable solvent quality to maintain consistent aroma formulations and production efficiency. AOLANSU provides batch-controlled supply with quality documentation support, helping flavor manufacturers reduce raw material evaluation time and improve production consistency.
For customers producing fruit flavors, beverage essences, bakery flavors, or aroma compounds, supply arrangements can be coordinated according to production schedules and consumption requirements.
Natural ingredient processors typically focus on solvent purity, extraction performance, and repeatability between batches. AOLANSU supports customers by providing controlled-quality solvent products suitable for botanical extraction and natural compound processing.
Technical specifications, documentation requirements, and supply frequency can be discussed according to the customer's extraction process and quality management procedures.
Large-scale food ingredient manufacturers require stable supply capacity to avoid production interruptions caused by raw material shortages or inconsistent quality. AOLANSU provides professional production management, batch traceability, and export coordination to support continuous procurement needs.
For regular purchasing projects, customers can communicate expected consumption volumes and delivery schedules to develop a suitable supply plan.
International buyers may require specific technical documents, quality records, and shipping information during supplier evaluation and import procedures. AOLANSU provides supporting documents such as Certificate of Analysis (COA), product specifications, and related technical information according to customer requirements.
With export experience and professional communication support, AOLANSU helps overseas customers simplify the sourcing process from product confirmation to shipment arrangement.
Store in tightly closed, suitable chemical containers in a cool, dry, and well-ventilated area. Keep away from direct sunlight, excessive heat, sparks, flames, and other ignition sources.
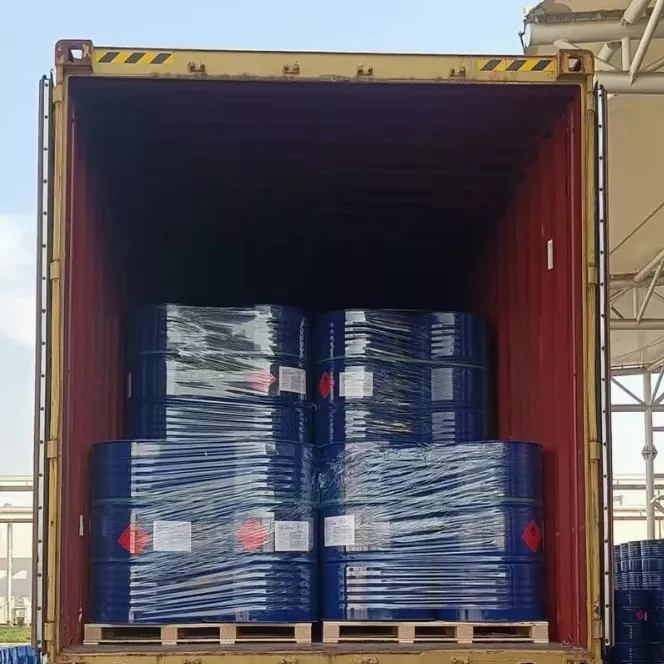
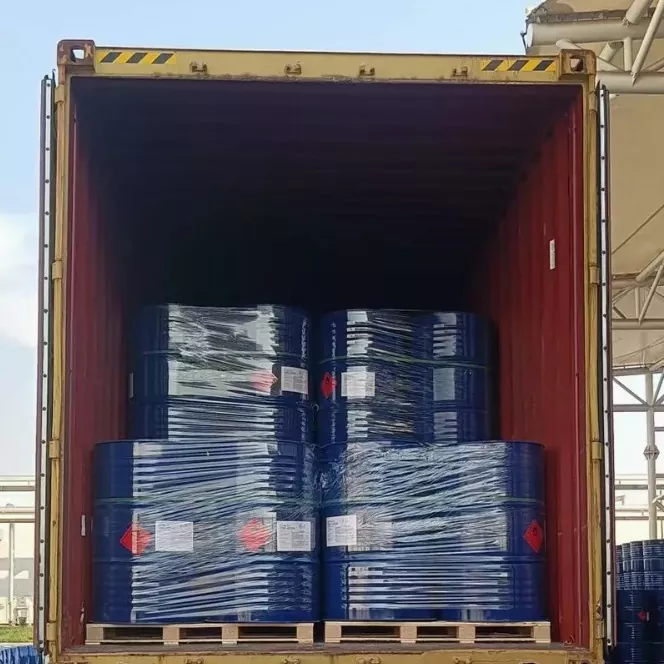
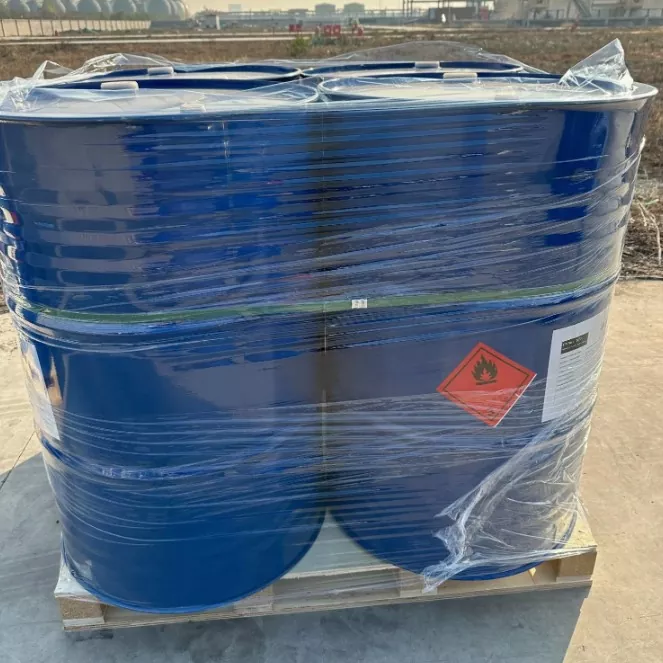
Transportation should follow the applicable requirements for flammable chemical products and the regulations of the destination market. Appropriate packaging, labeling, handling, and transportation procedures should be maintained throughout delivery.
Containers should remain properly sealed when the product is not being used. Good container management helps reduce contamination and unnecessary exposure to moisture during storage and production handling.
AOLANSU can provide Certificate of Analysis (COA) and relevant product quality information according to customer requirements. Documentation can include key parameters such as purity, moisture, acidity, and other specification data.
Batch-related production and testing records support traceability from manufacturing through shipment. This can help customers manage incoming inspection and maintain their own raw material quality records.
AOLANSU supports international customers with product specifications, technical communication, documentation, packaging coordination, and shipment arrangements. The supply process can be adapted to different order quantities and destination requirements.
It is mainly used in flavor extraction, aroma formulation, natural ingredient extraction, beverage flavor processing, coffee and tea processing, and other applications requiring a high-purity solvent with controlled quality characteristics.
The main difference is the quality and application requirements. Food-related applications generally require tighter control of purity, moisture, acidity, residual matter, odor characteristics, and other impurities. Industrial-grade material is primarily intended for applications such as coatings, printing inks, adhesives, and general solvent use.
Solvent purity can affect extraction performance, residual behavior, odor, and potential flavor interference. Consistent quality is therefore important for manufacturers producing flavor systems with defined sensory characteristics.
Yes. It can function as an extraction or carrier solvent for selected aroma compounds and natural flavor components. Customers should confirm process compatibility and applicable food regulations for their specific application.
Yes. AOLANSU can provide COA and relevant product quality documentation according to the customer's purchasing and documentation requirements.
AOLANSU can supply food-compatible HDPE drums, IBC containers, and suitable bulk transportation formats. The appropriate packaging can be selected according to order volume, destination, and transportation conditions.
It should be kept in sealed containers in a cool, dry, well-ventilated location and protected from heat, sunlight, flames, sparks, and other ignition sources. Storage should comply with applicable chemical safety requirements.
Yes. AOLANSU supports international customers with product documentation, quality verification, packaging coordination, export service, and logistics arrangements.
AOLANSU focuses on high-purity chemical manufacturing and provides solvent solutions for food processing, flavor manufacturing, natural ingredient extraction, and related industries.
Purification, laboratory testing, and batch traceability procedures help maintain consistent product characteristics and provide customers with measurable quality information.
AOLANSU holds a Hazardous Chemicals Business License, supporting compliant chemical business operations and professional handling of relevant chemical products.
With drum, IBC, and bulk supply options together with export documentation and logistics coordination, AOLANSU can support both regular purchasing and larger-volume sourcing requirements.
If you are sourcing a reliable Food Grade Ethyl Acetate supplier in China for flavor production, natural ingredient extraction, beverage processing, or coffee and tea applications, AOLANSU can provide product specifications, COA documentation, packaging options, and international supply support.
Contact AOLANSU with your required purity, annual consumption, packaging preference, destination market, and application details to discuss a suitable supply solution.
Address
(North of Dongwei Group, West) Houwei Village, Changshan Town, Zouping City, Binzhou, Shandong Province, China
Tel