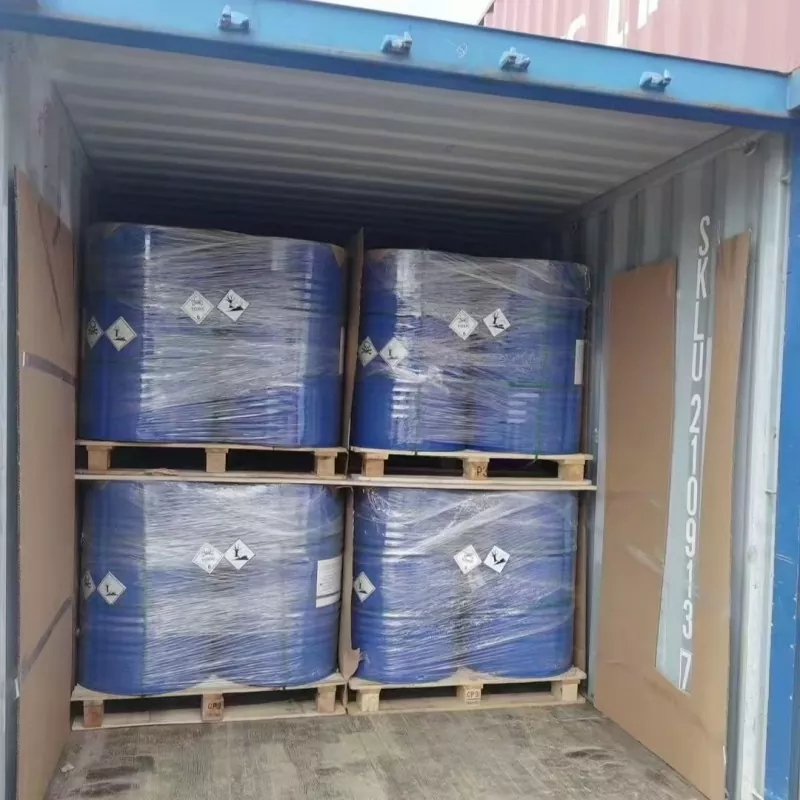
For chemical buyers, selecting an ether product is not simply a matter of reaching a target purity. Batch stability, impurity control, documentation, packaging, and supplier compliance can all affect downstream production and procurement efficiency. AOLANSU provides high-purity Methyl Tert-Butyl Ether 99.9% with a nominal purity of ≥99.9%, supported by laboratory testing and technical documentation for customers with controlled chemical-material requirements.
The product is supplied by Shandong Aolansu Environmental Protection Technology Co., Ltd. and is intended for specialty chemical processing, laboratory research, fine chemical applications, and other processes where consistent chemical characteristics are important. Typical supporting documents include COA, SDS, and product specifications.
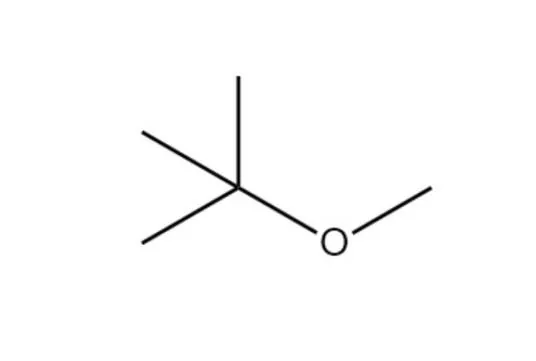
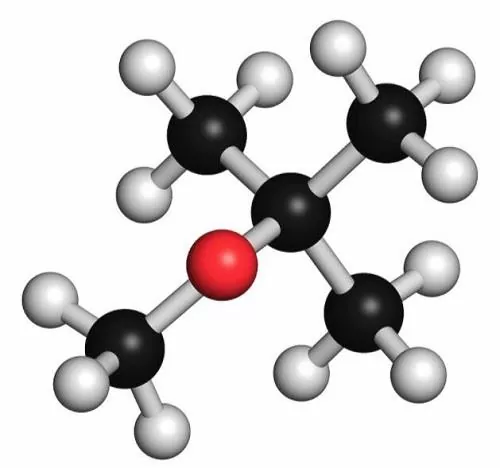
When purchasing high-purity chemical materials, the actual purchasing risk often comes from inconsistent batches rather than the nominal specification alone. Differences in moisture, methanol content, impurity levels, or documentation can create additional work during incoming inspection and process verification.
AOLANSU addresses these requirements through batch testing, quality documentation, and controlled supply procedures. This gives buyers clearer information for supplier qualification, incoming quality checks, and internal chemical management.
The Methyl Tert-Butyl Ether 99.9% purity specification is supported by gas chromatography analysis. Other controlled indicators include methanol and water content, allowing customers to evaluate the material according to more than a single purity figure.
For processes where raw-material consistency influences reaction conditions or formulation results, maintaining a controlled impurity profile can help reduce variation between incoming batches.
Before delivery, each batch undergoes laboratory analysis covering purity, moisture, impurity control, appearance, and other relevant quality parameters. The corresponding documentation can support customer-side incoming inspection and material verification.
This approach is particularly useful for buyers who need to maintain internal records for repeated chemical procurement rather than treating every order as an isolated purchase.
The typical specification provided by AOLANSU includes the following parameters. Customized requirements can be discussed according to the intended application.
| Parameter | Specification | Test Method |
|---|---|---|
| Product Name | Methyl Tert-Butyl Ether (MTBE) | — |
| CAS Number | 1634-04-4 | — |
| Purity | ≥99.9% | Gas Chromatography |
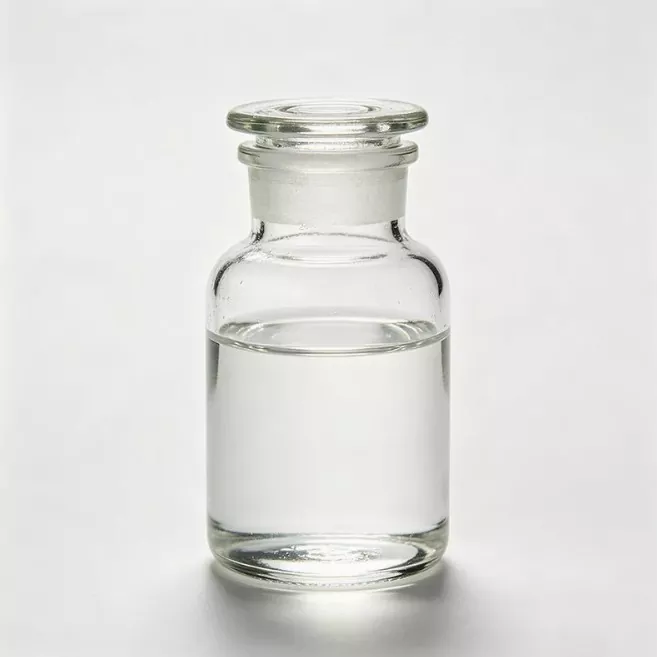
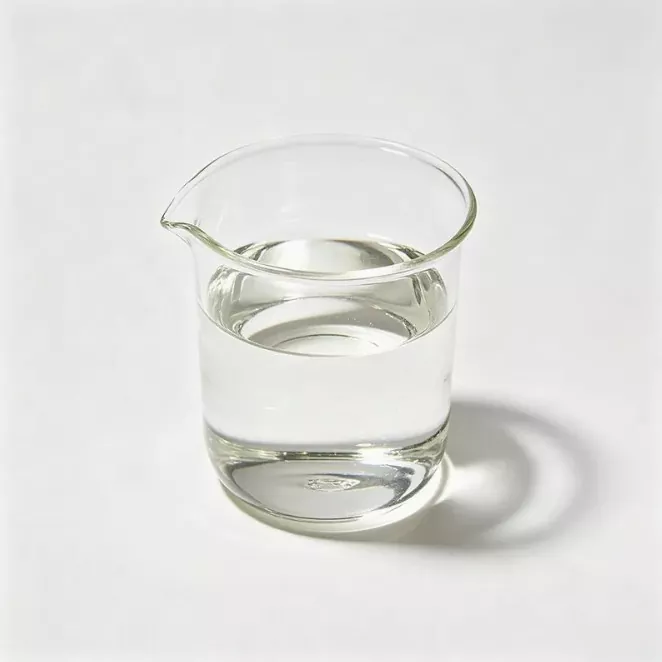
| Appearance | Clear Colorless Transparent Liquid | Visual Inspection |
| MTBE Content | ≥99.9% | GC Analysis |
| Methanol Content | ≤0.02% | Gas Chromatography |
| Water Content | ≤0.05% | Karl Fischer Method |
| Density at 20℃ | 0.740–0.745 g/cm³ | Density Measurement |
| Boiling Point | 55–56℃ | Standard Test Method |
| Acidity | ≤0.005% | Titration Method |
| Non-Volatile Matter | Controlled According to Specification | Evaporation Method |
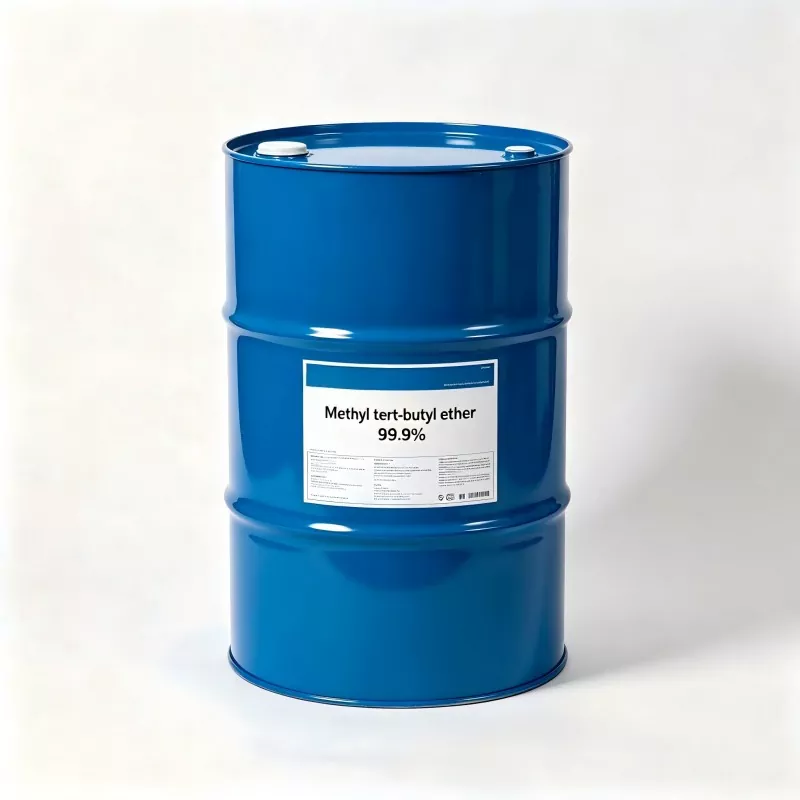
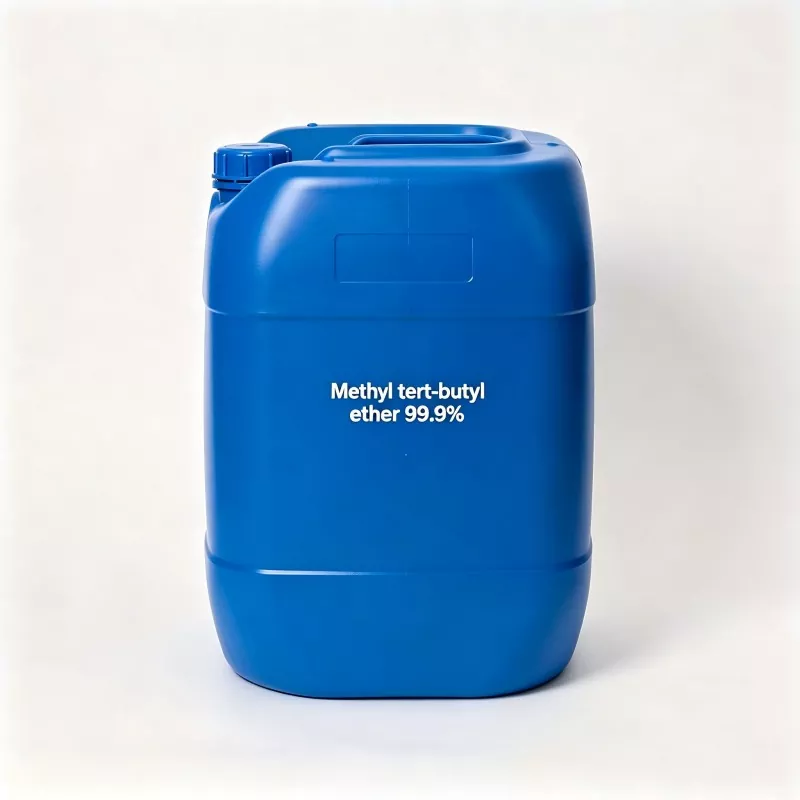
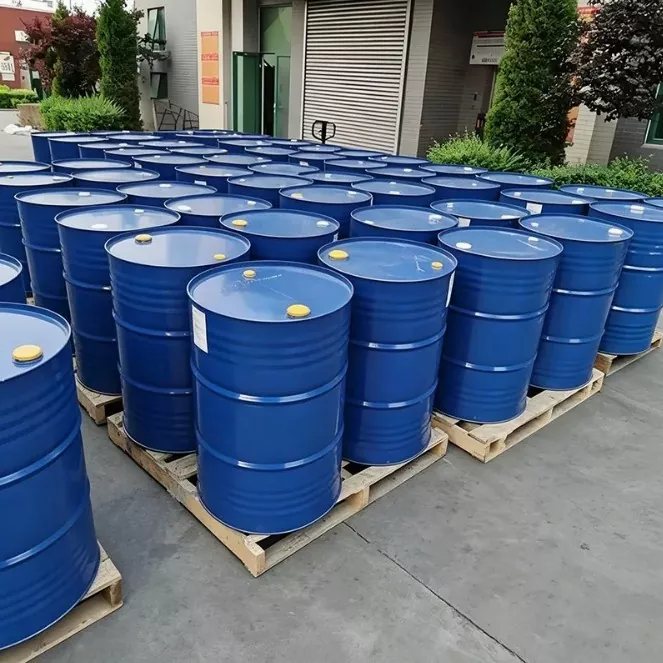
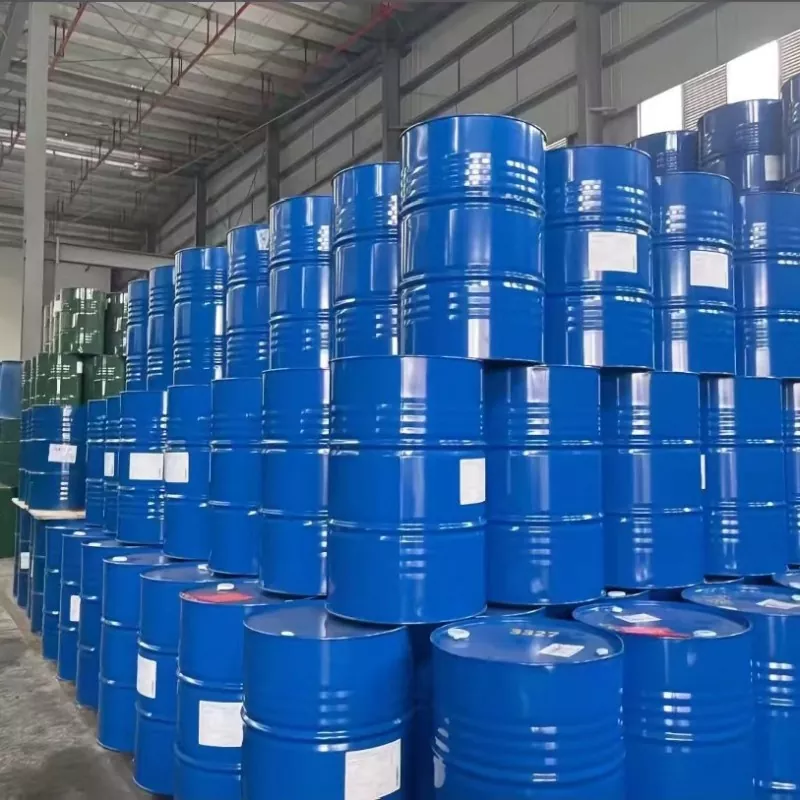
| Packaging | Drum / ISO Tank / Customized Packaging | Customer Requirement |
| Storage | Cool, Dry and Well-Ventilated Area | — |
The material can be selected for specialty chemical processes involving controlled ether-based chemical characteristics. Its stated purity and controlled composition make it suitable for synthesis and formulation development where raw-material consistency is important.
For laboratories and research teams, consistent composition is important when performing chemical analysis, testing, and experimental work. The high-purity specification provides a defined material quality for applications requiring controlled chemical inputs.
Fine chemical and pharmaceutical-related production may require raw materials with clearly defined specifications and supporting documentation. This grade can be considered for specialized processes where purity control and material consistency are purchasing priorities.
Certain industrial formulations require tighter control over raw-material characteristics than general-purpose manufacturing. In these situations, a high-purity ether material can provide a more controlled starting material for formulation and processing requirements.
A reliable chemical supplier needs to provide more than the product itself. AOLANSU applies standardized production procedures and monitors key product indicators during manufacturing and inspection. Batch-related documentation includes COA, SDS, and product specifications, helping customers complete supplier evaluation and internal material-management procedures.
For international procurement, AOLANSU can also provide product information, safety documentation, shipping coordination, and other support required during chemical purchasing and delivery.
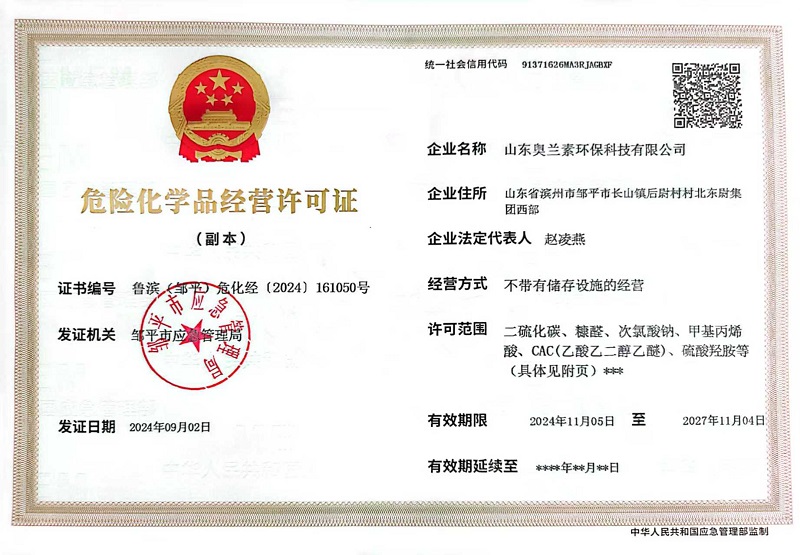
Methyl Tert-Butyl Ether belongs to a category of chemicals for which procurement, storage, transportation, and handling require appropriate safety and compliance management. Shandong Aolansu Environmental Protection Technology Co., Ltd. holds a valid Hazardous Chemical Business License issued by the local emergency management authority, supporting its qualified hazardous chemical operation and supply capability.
For overseas buyers, this qualification can be an important part of supplier assessment, particularly when procurement departments need to verify the supplier's ability to manage regulated chemical products.
Not every MTBE purchasing requirement calls for the same grade. The appropriate choice depends on purity requirements, process sensitivity, intended application, and procurement objectives.
The 99.9% grade is positioned for applications where higher purity, impurity control, and batch consistency are important. Industrial-grade material is more suitable for general manufacturing requirements, while fuel-grade MTBE is primarily associated with gasoline blending and fuel-production applications.
For buyers comparing suppliers, it is therefore useful to evaluate the complete specification and quality-control system instead of comparing only the quoted unit price.
A specialty chemical manufacturer was looking for a supplier capable of providing stable purity, consistent batch quality, and complete technical documentation for its production process.
After evaluating different suppliers, the customer selected AOLANSU's high-purity material because of its quality-control system and professional chemical supply support. During regular cooperation, the customer achieved improved raw-material consistency and more reliable production management.
This case demonstrates why chemical procurement decisions often depend on the combination of product specifications, batch control, documentation, and supply support rather than purity alone.
It is mainly intended for applications requiring high chemical purity and stable composition, including specialty chemical synthesis, laboratory research, fine chemical processing, and selected industrial formulations.
The key difference is the required purity and degree of quality control. The 99.9% grade is intended for applications with stricter chemical consistency requirements, while industrial grades generally focus on practical performance and large-scale industrial supply.
Yes. COA, SDS, technical specifications, and related quality documents can be supplied according to customer requirements.
Quality is controlled through standardized production management, laboratory analysis, batch inspection, and documentation control before shipment.
Drum, ISO Tank, and customized packaging options are available according to customer requirements, transportation conditions, and order quantity.
Yes. The company provides export documentation, logistics coordination, and shipment support for international chemical procurement.
The selection should be based on the actual process and quality requirements. Buyers needing higher purity and stricter impurity control can consider the 99.9% grade, while general industrial applications may use industrial-grade material.
AOLANSU combines chemical supply experience with production management, laboratory testing, documentation support, and hazardous chemical operation qualifications. The company provides technical communication and assistance from product inquiry through documentation and shipment coordination.
For buyers looking for a long-term chemical supply partner, the focus is not only on meeting the stated specification but also on maintaining consistent batches, providing traceable quality information, and supporting the practical requirements of international procurement.
Address
(North of Dongwei Group, West) Houwei Village, Changshan Town, Zouping City, Binzhou, Shandong Province, China
Tel