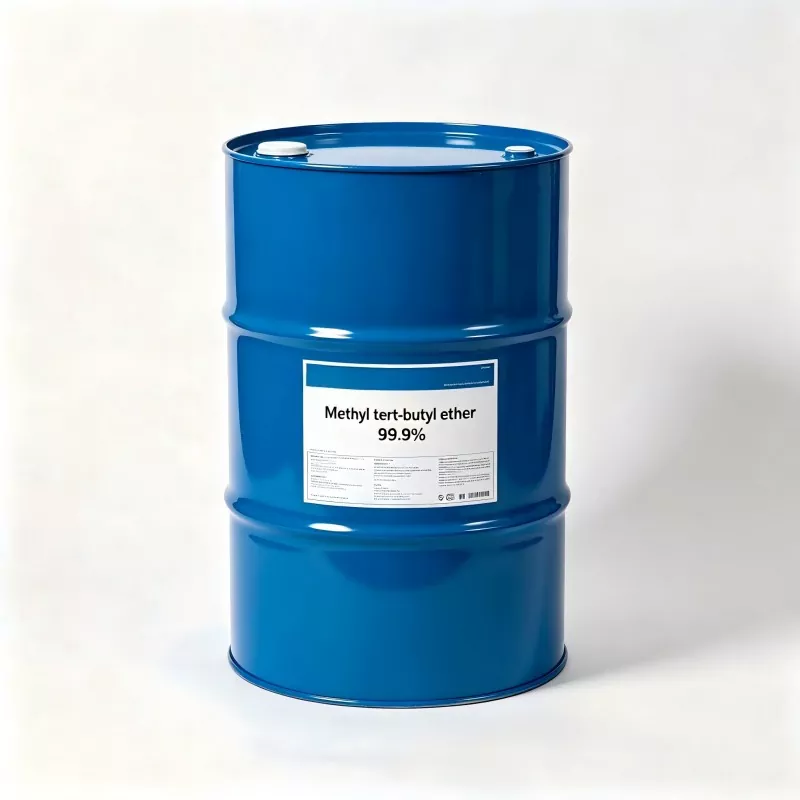
For fuel manufacturers, petroleum companies, and chemical enterprises, selecting a reliable chemical supplier involves more than product performance. Supply stability, compliance capability, quality consistency, and long-term cooperation ability are also critical factors. Industrial Grade Methyl Tert-Butyl Ether is an important chemical material widely used in gasoline blending, petroleum processing, and industrial applications due to its stable chemical characteristics and reliable performance.
Shandong Aolansu Environmental Protection Technology Co., Ltd. specializes in supplying Industrial Grade MTBE for global customers. With professional chemical supply experience, standardized management processes, and strict quality control procedures, AOLANSU provides consistent products and reliable delivery solutions for fuel producers, petroleum companies, chemical manufacturers, and industrial users.
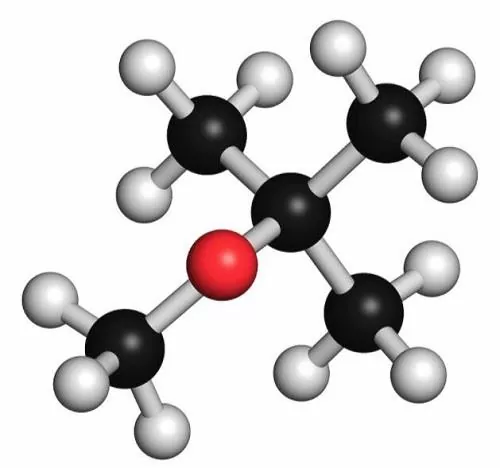
For international buyers, maintaining a stable supply chain is essential for continuous production. AOLANSU focuses on providing dependable chemical procurement solutions to help customers reduce supply risks, improve purchasing efficiency, and establish long-term cooperation relationships.
For industries using chemical materials in large-scale production, consistent quality directly affects production efficiency and final product performance. Unstable raw material quality may increase production adjustments and operational costs.
AOLANSU controls the manufacturing process through standardized procedures and strict inspection systems. Each batch of Industrial Grade Methyl Tert-Butyl Ether is carefully tested to ensure reliable quality consistency, allowing customers to maintain stable production processes and reduce quality-related risks.
Fuel and chemical industries usually require continuous raw material supply to support long-term operations. A supplier with strong production coordination and logistics capability can help customers maintain smoother procurement cycles.
AOLANSU provides flexible supply solutions according to customer requirements, including bulk orders, ISO tank transportation, and customized shipment arrangements. Through professional supply management and export experience, AOLANSU helps global customers establish reliable MTBE supply channels.
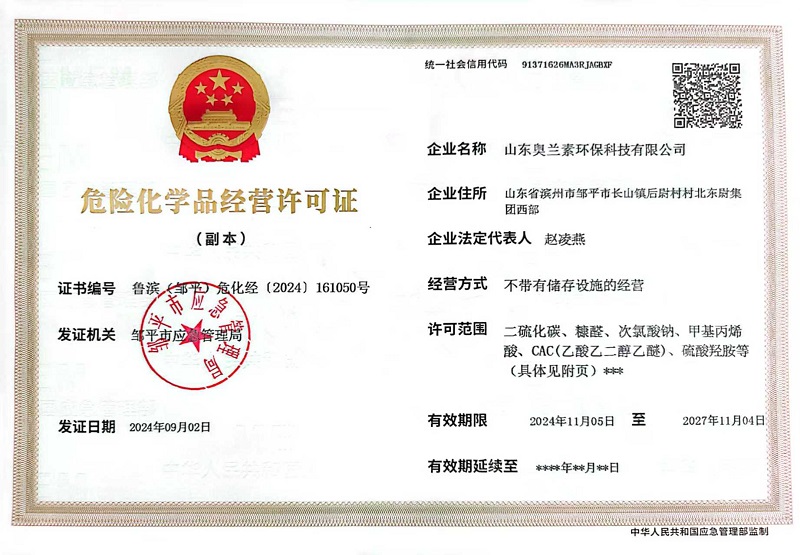
For chemical buyers, supplier qualification and compliance ability are important considerations during procurement. AOLANSU holds a valid Hazardous Chemical Business License, demonstrating its capability in hazardous chemical operation, product management, and international chemical supply services.
With professional documentation support, product information management, and shipment coordination, AOLANSU helps customers complete chemical purchasing procedures more efficiently and safely.
One of the major applications of Industrial Grade MTBE is gasoline blending. As an oxygenated compound, MTBE helps improve octane performance and supports fuel formulation optimization.
Fuel manufacturers use MTBE as a blending component to improve gasoline quality and achieve more stable combustion characteristics according to production requirements.
In petroleum refining operations, MTBE is commonly used as a chemical additive in fuel production processes. Its stable properties make it suitable for large-scale refinery applications where reliable chemical performance is required.
A continuous MTBE supply enables petroleum companies to maintain production schedules and reduce the impact caused by raw material shortages.
Besides fuel-related industries, Industrial Grade Methyl Tert-Butyl Ether can also be used as an industrial chemical material in different manufacturing processes. Its compatibility and stable characteristics allow it to meet the requirements of various industrial applications.
Companies requiring ether-based chemical solutions can select MTBE according to their production processes and technical requirements.
MTBE can be applied in industrial scenarios where chemical stability and compatibility are required. With suitable storage, transportation, and handling procedures, it can support different industrial users with reliable material solutions.
For chemical products, proper storage and transportation management are essential to maintain product quality and ensure safe delivery. MTBE has specific requirements for handling, storage environment, and transportation conditions, making supplier experience an important factor for international procurement.
AOLANSU provides professional supply coordination according to customer delivery requirements. From product preparation and packaging selection to transportation arrangements, AOLANSU supports customers with reliable logistics solutions to ensure that products arrive safely and efficiently.
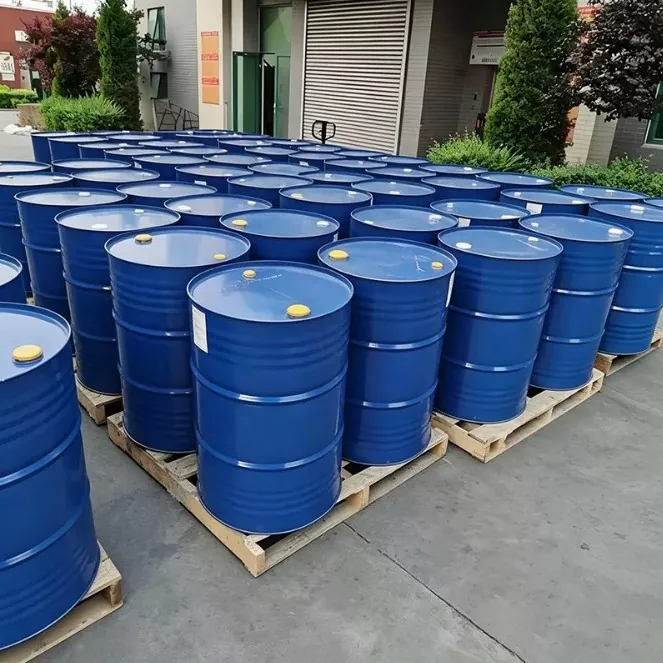
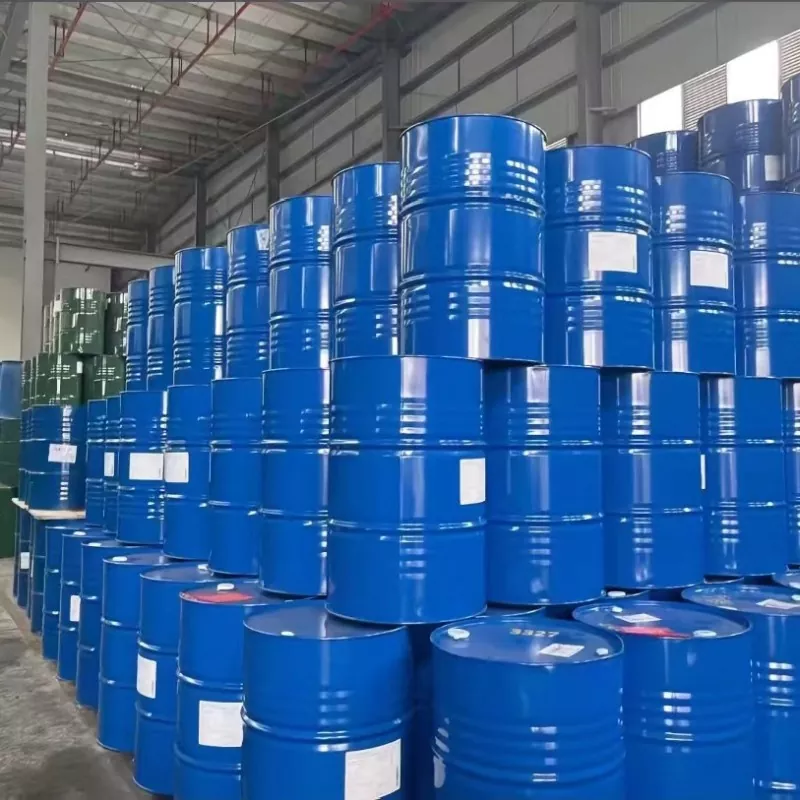
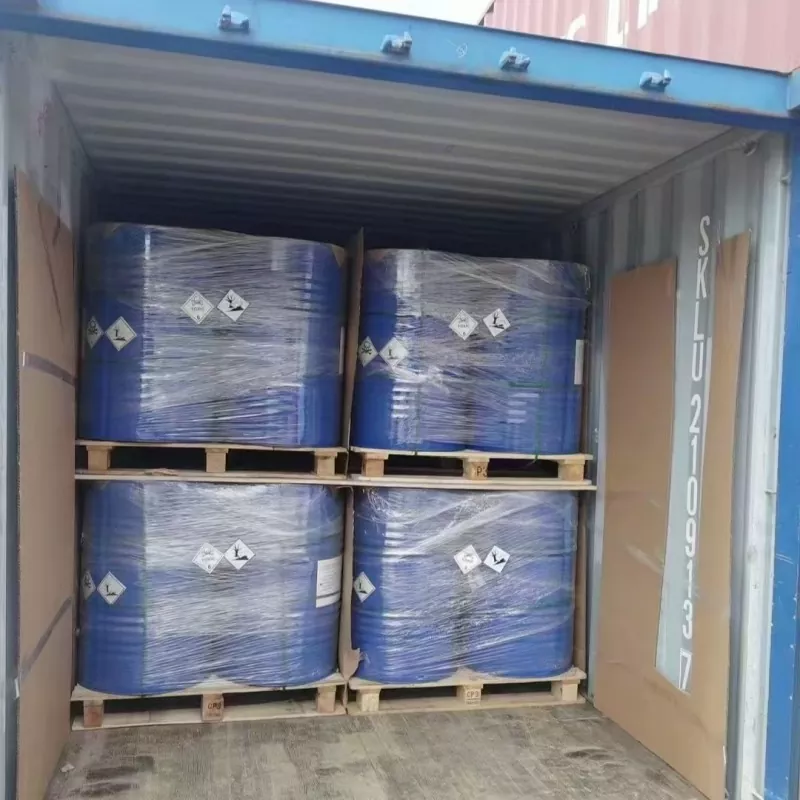
For bulk procurement, AOLANSU can provide suitable packaging options including ISO tanks, bulk shipment solutions, and industrial drums. These flexible delivery methods allow customers from different industries to select the most appropriate transportation solution according to order volume and application requirements.
With professional export experience and chemical management capability, AOLANSU helps global customers improve procurement efficiency and maintain stable supply operations.
For industrial users, choosing a chemical supplier involves evaluating not only product quality but also supplier reliability, compliance ability, and service support. A stable supplier can help companies reduce unexpected production interruptions and improve supply chain management.
AOLANSU provides comprehensive support throughout the purchasing process, including product information confirmation, technical document preparation, shipment coordination, and communication support. This service approach helps customers complete procurement procedures more smoothly.
Through strict quality management and professional chemical supply experience, AOLANSU works with customers to establish long-term cooperation based on reliable products and efficient service.
The following specifications represent typical Industrial Grade Methyl Tert-Butyl Ether quality standards supplied by AOLANSU. Customized specifications can be discussed according to customer application requirements.
| Parameter | Specification |
|---|---|
| Chemical Name | Methyl Tert-Butyl Ether (MTBE) |
| CAS Number | 1634-04-4 |
| Appearance | Colorless Transparent Liquid |
| Purity | ≥99.0% |
| MTBE Content | ≥99.0% |
| Methanol Content | ≤0.05% |
| Water Content | ≤0.10% |
| Density (20℃) | 0.740-0.745 g/cm³ |
| Boiling Point | 55-56℃ |
| Flash Point | -28℃ |
| Acidity | Controlled According to Specification |
| Packaging | ISO Tank / Bulk Shipment / Drum |
| Shelf Life | 12 Months |
Stable chemical performance depends on effective production management. AOLANSU monitors raw materials, production conditions, and finished products throughout the manufacturing process to maintain reliable quality.
Through systematic quality control procedures, AOLANSU ensures that each batch meets customer requirements and provides consistent performance for industrial applications.
Before shipment, every batch of Industrial Grade MTBE undergoes professional laboratory testing. Key indicators such as purity, moisture content, appearance, and chemical characteristics are evaluated to ensure product reliability.
Complete inspection procedures provide customers with greater confidence when purchasing chemical products for large-scale industrial use.
International chemical procurement requires complete technical and shipping documents. AOLANSU provides customers with professional documentation support, including Certificate of Analysis (COA), product specifications, and related export documents.
These services help customers complete supplier evaluation, import procedures, and internal quality management more efficiently.
A regional fuel company was searching for a reliable MTBE supplier to support continuous gasoline blending operations. The customer required stable product quality, consistent delivery schedules, and professional export support.
After cooperating with Shandong Aolansu, the customer received regular Industrial Grade MTBE shipments with consistent specifications and reliable logistics coordination. The stable supply system helped the customer maintain production planning and reduce raw material procurement risks.
Through continuous communication and dependable delivery performance, AOLANSU established a long-term supply partnership with the customer.
Industrial Grade Methyl Tert-Butyl Ether is mainly used in gasoline blending, petroleum processing, chemical manufacturing, and other industrial applications requiring reliable ether-based chemical materials.
MTBE is used in gasoline blending because it can improve octane performance and provide oxygen content for fuel formulations. It helps fuel manufacturers optimize gasoline quality and combustion efficiency.
Industrial Grade MTBE is designed for large-scale industrial applications where stable supply, reliable performance, and procurement efficiency are important. High Purity MTBE is mainly used for applications requiring stricter purity control.
Industrial Grade MTBE refers to MTBE products supplied for broad industrial requirements, including fuel-related applications and chemical processing. Fuel Grade MTBE focuses more specifically on fuel blending standards and gasoline performance requirements.
Yes. AOLANSU supports bulk MTBE supply through ISO tanks, bulk transportation, and other suitable packaging solutions according to customer order volume and transportation requirements.
Yes. AOLANSU provides international chemical export services, including documentation support, logistics coordination, and shipment arrangements.
Yes. Packaging solutions can be adjusted according to customer transportation conditions, storage requirements, and order quantity.
If you are looking for a reliable Industrial Grade Methyl Tert-Butyl Ether supplier in China, Shandong Aolansu Environmental Protection Technology Co., Ltd. can provide stable product quality, professional hazardous chemical operation capability, flexible supply solutions, and international delivery support.
With a focus on quality control, compliance management, and long-term cooperation, AOLANSU helps global customers build reliable chemical supply partnerships.
Address
(North of Dongwei Group, West) Houwei Village, Changshan Town, Zouping City, Binzhou, Shandong Province, China
Tel