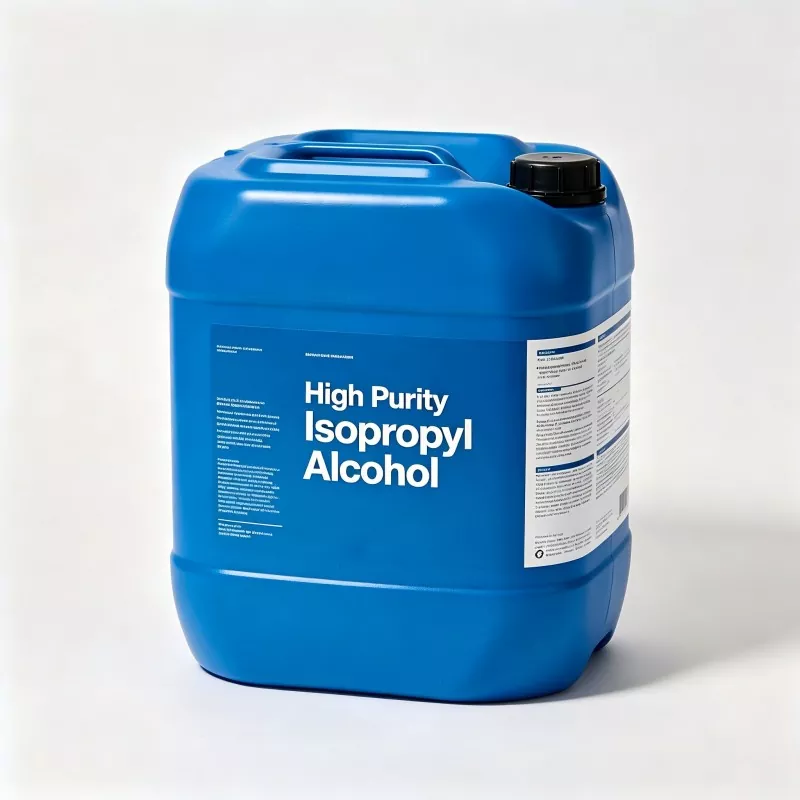
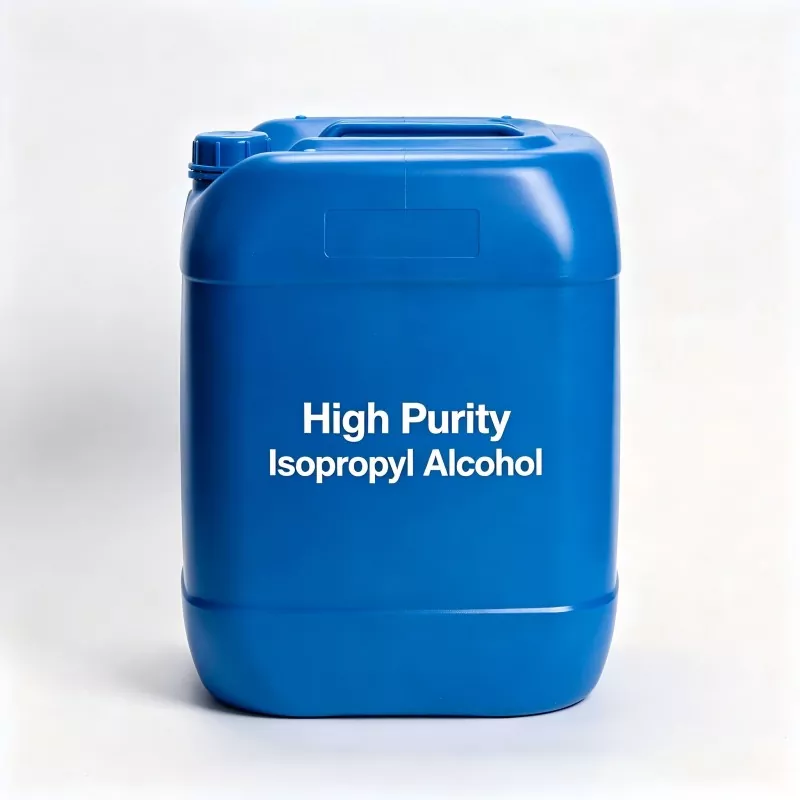
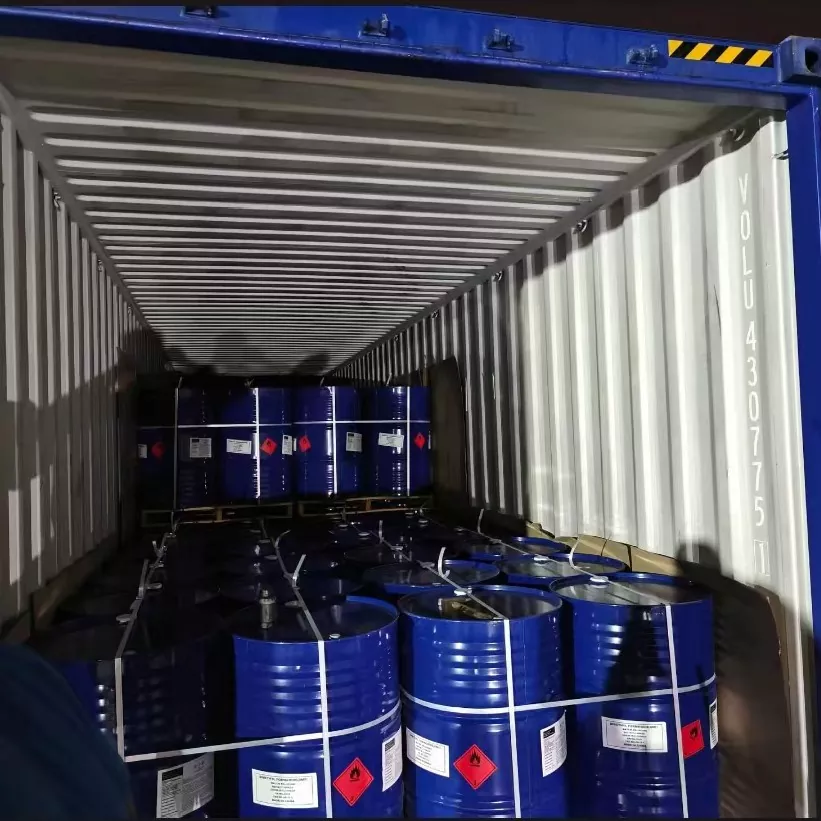
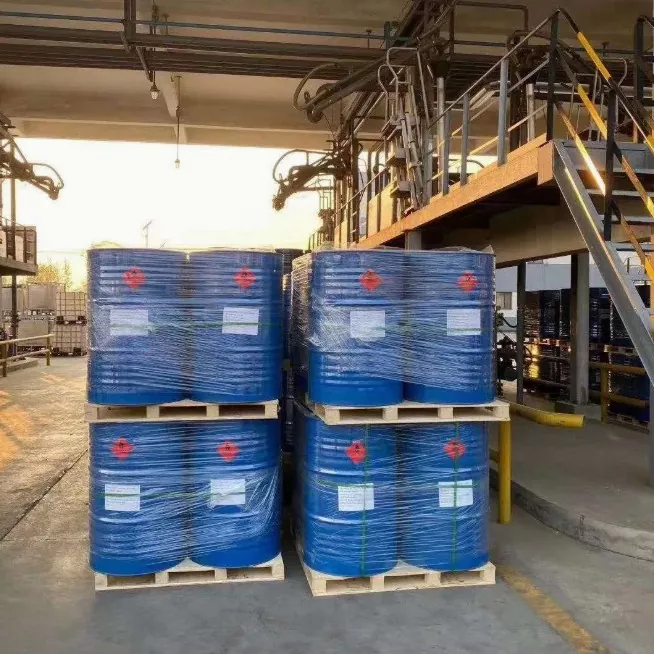
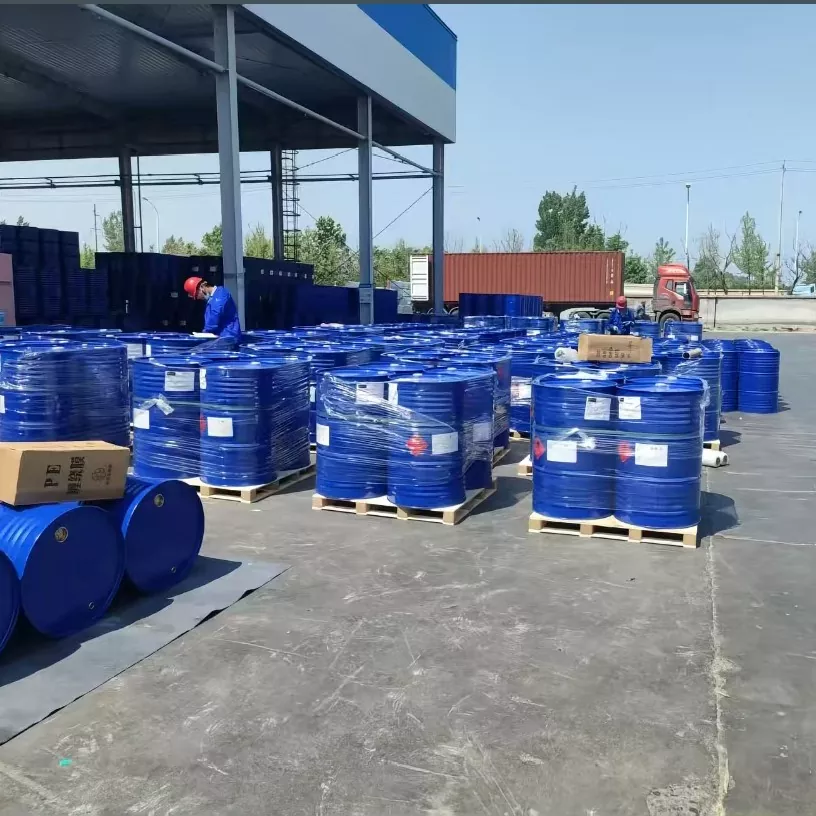
In precision manufacturing, solvent purity is not simply a specification—it can directly influence surface cleanliness, process stability, and final product reliability. For applications involving semiconductor components, optical parts, laboratory instruments, and sensitive electronic materials, even trace moisture, particles, or ionic contaminants may create unexpected process risks. AOLANSU High Purity Isopropyl Alcohol is developed for these cleanliness-sensitive applications, with controlled impurity levels and batch testing designed to provide consistent solvent performance.
Shandong Aolansu Environmental Technology Co., Ltd. is a professional China chemical manufacturer and supplier based in Binzhou, Shandong. Established in 2020, AOLANSU provides high-purity solvent solutions for semiconductor manufacturing, precision electronics, pharmaceutical processing, optical cleaning, and laboratory applications. The company also holds a hazardous chemical business license and provides professional documentation and export support for international customers.
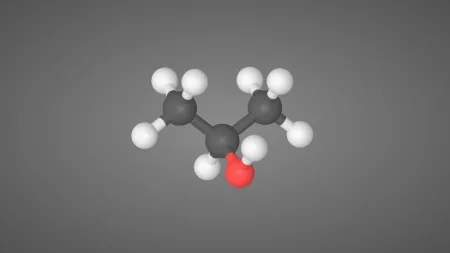
For general industrial cleaning, solvent purity may be evaluated mainly by concentration. Precision applications require a much broader quality assessment. Moisture, trace metals, particles, non-volatile residues, packaging cleanliness, and batch-to-batch consistency can all affect the final process result.
AOLANSU High Purity Isopropyl Alcohol is therefore controlled through multiple quality parameters rather than relying on purity alone. The production process incorporates purification, dehydration, fine filtration, controlled filling, and analytical inspection to reduce contamination risks throughout production and packaging.
Selected raw materials undergo controlled purification and rectification processes before the finished solvent is prepared. Dehydration and fine filtration are used to reduce unwanted moisture, organic residues, particles, and other contaminants that may interfere with precision manufacturing processes.
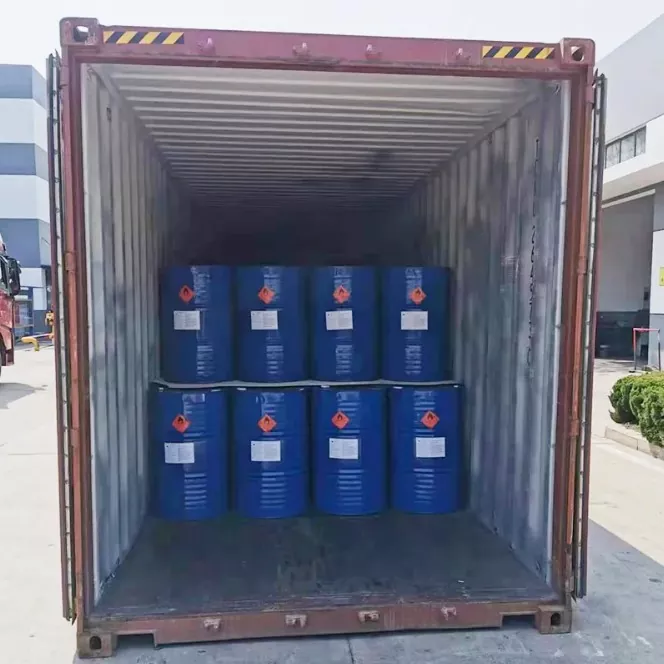
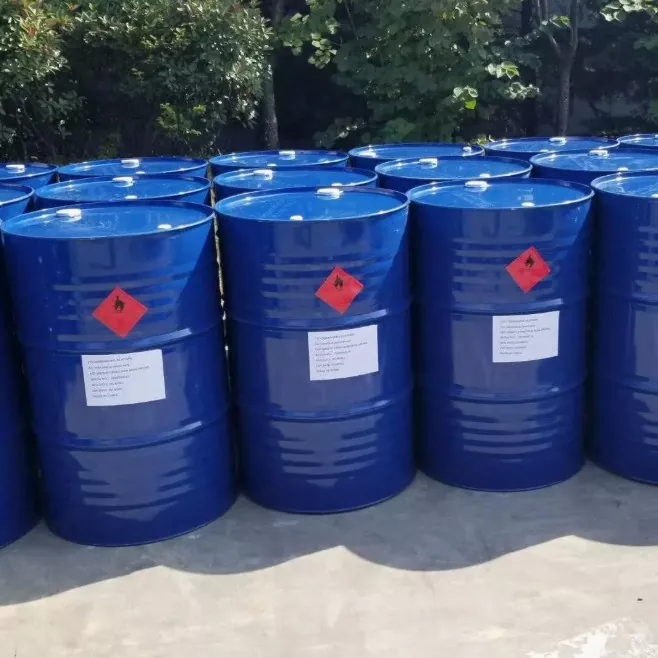
High-purity solvent performance can be compromised after production if inappropriate containers or handling procedures are used. AOLANSU applies sealed filling procedures and suitable packaging solutions to minimize exposure to external contamination during storage and transportation.
Each production batch is subject to laboratory testing before shipment. Quality records can cover purity, moisture, trace metals, particle levels, and residue indicators. A Certificate of Analysis (COA) is available to help customers verify the delivered material against their purchasing specifications.
Trace metallic contamination is a critical concern in semiconductor and precision electronic processes. AOLANSU High Purity Isopropyl Alcohol is designed with controlled levels of metallic impurities, including sodium, potassium, calcium, iron, and copper. This helps reduce contamination risks when the solvent is used on sensitive components or manufacturing equipment.
Moisture can influence cleaning efficiency, drying behavior, and material compatibility. With a specified water content of ≤0.01%, the product is suitable for processes where moisture control is an important part of solvent selection.
After evaporation, solvent residue may remain on sensitive surfaces if the material contains excessive non-volatile impurities. The specified evaporation residue of ≤0.0001% helps support cleaner surfaces in precision cleaning applications.
Particles are particularly important when cleaning wafers, optical components, and precision electronic parts. The specified particle control of ≤10 particles/mL for particles ≥0.5 μm provides a defined cleanliness target for applications requiring controlled particulate levels.
High-purity IPA is commonly used for wafer surface cleaning, process equipment cleaning, and removal of selected organic contaminants. Its volatility and low-residue characteristics make it suitable for processes where surface cleanliness must be maintained between manufacturing steps.
Electronic manufacturers can use the solvent for removing flux residues, fingerprints, oils, and other organic contaminants from components and production equipment. Controlled impurity levels help minimize the risk of introducing unwanted contaminants during cleaning.
Optical lenses, precision instruments, and selected optical components require cleaning methods that minimize residue and surface contamination. High-purity IPA can be used as a cleaning solvent where controlled evaporation and low residue are required.
The product can be used as a solvent or cleaning material in pharmaceutical processing, laboratory work, and equipment maintenance where consistent solvent quality and traceable documentation are important. The required grade should always be selected according to the specific application and applicable regulations.
A semiconductor component manufacturer in East Asia previously experienced unstable cleaning results caused by solvent residue and inconsistent impurity levels. After switching to AOLANSU high-purity solvent products, the customer achieved a more stable cleaning process, reduced surface residue, and improved consistency during repeated wafer handling procedures.
In electronic assembly applications, customers use the solvent to remove flux residues and surface contaminants from sensitive components. The low-residue characteristics support clean component surfaces while minimizing the potential impact on delicate electronic materials.
| Parameter | Specification | Test Method |
|---|---|---|
| Purity | ≥99.9% | GC |
| Water Content | ≤0.01% | Karl Fischer |
| Evaporation Residue | ≤0.0001% | Gravimetric Analysis |
| Total Metal Content | ≤1 ppb | ICP-MS |
| Particle Control | ≤10 particles/mL (≥0.5 μm) | Laser Particle Counter |
| Color | ≤5 APHA | ASTM D1209 |
| Storage Stability | 24 months under proper conditions | - |
| Packaging | 1L / 4L / 20L / 200L HDPE containers, IBC | Export Standard |
Purity alone does not fully describe a high-purity solvent. A material can meet a nominal purity value while still requiring control of moisture, particles, trace metals, and non-volatile residues. Buyers should therefore review the complete specification and COA rather than comparing only the main purity percentage.
Packaging can affect solvent cleanliness after purification. Containers that are unsuitable for high-purity chemicals may introduce particles or contaminants during storage. For sensitive applications, customers should select compatible packaging and keep containers tightly sealed until use.
Cleaning results are also affected by application temperature, contact time, wiping materials, equipment condition, substrate compatibility, and drying conditions. When process results fluctuate, manufacturers should evaluate the complete cleaning process instead of replacing the solvent immediately.
Different industries have different contamination-control requirements. Semiconductor, optical, electronics, pharmaceutical, and laboratory applications may require different specifications. Before bulk purchasing, buyers should confirm critical parameters such as moisture, particles, metal ions, residue, and packaging requirements.
AOLANSU manages solvent production according to controlled operating procedures covering raw material handling, purification, storage, filling, and transportation. The production process is designed to reduce unnecessary material loss while maintaining stable product quality.
Isopropyl alcohol is a flammable chemical, so production, storage, and transportation require appropriate safety controls. AOLANSU holds a hazardous chemical business license and follows applicable requirements for hazardous chemical management, storage, labeling, and transportation.
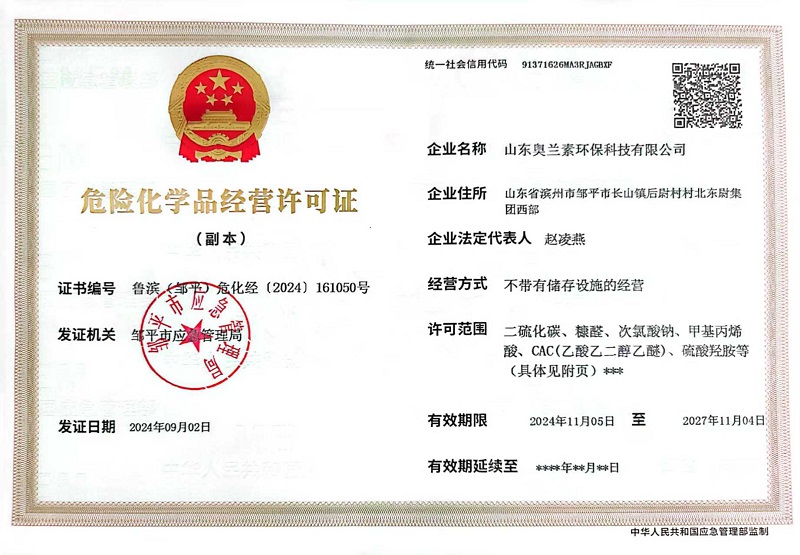
Production and storage areas are managed with measures appropriate for flammable solvents, including ventilation, fire prevention, equipment inspection, and operating procedures. Personnel handling the material receive relevant safety training and follow established chemical handling requirements.
Suitable sealed containers are selected according to the order quantity and transportation method. Export shipments are supported with product documentation such as SDS, COA, specifications, and applicable dangerous goods shipping documents to help customers manage transportation and import procedures.
Shandong Aolansu Environmental Technology Co., Ltd. operates a chemical production facility in Binzhou, Shandong, China, with a focus on solvent products for industrial and precision applications. Production procedures are organized to maintain stable quality from raw material selection through finished product packaging.
Professional analytical methods are used to monitor key quality indicators. Depending on customer requirements, testing can include gas chromatography, Karl Fischer moisture analysis, ICP-MS trace metal analysis, and particle inspection.
For international orders, AOLANSU can provide COA, SDS, product specifications, shipping documents, and other relevant technical information. These documents allow distributors and industrial users to verify incoming material and maintain internal quality records.
Different packaging formats are available according to application and logistics requirements, including HDPE containers, drums, IBC tanks, and bulk transportation solutions. The appropriate packaging should be selected according to order volume, storage conditions, transportation requirements, and contamination-control expectations.
As a China-based chemical supplier, AOLANSU supports international customers with order coordination, documentation preparation, logistics communication, and shipment arrangements. This provides buyers with a more complete procurement process from product specification confirmation to delivery.
The primary difference is contamination control. General industrial IPA is commonly used for cleaning, degreasing, and solvent applications, while high-purity grades require much tighter control of moisture, particles, trace metals, and non-volatile residues. These parameters are particularly important in semiconductor, electronics, optical, and other precision manufacturing processes.
Typical applications include semiconductor processing, precision electronics, optical component cleaning, pharmaceutical processing, laboratory work, and high-cleanliness equipment maintenance. The appropriate specification depends on the customer's process and contamination-control requirements.
AOLANSU uses standardized production procedures and batch-level analytical testing. Key indicators such as purity, moisture, residue, particles, and trace metals can be evaluated before shipment. COA documentation is available for customers to review the quality parameters of each batch.
Yes. AOLANSU can discuss different packaging formats and quantities according to customer requirements, including small containers, HDPE drums, IBC packaging, and bulk supply. Packaging selection can also take into account transportation distance and contamination-control requirements.
Customers can provide their application requirements and target specifications before ordering. AOLANSU can evaluate parameters such as purity, moisture, trace metals, particles, residue, and packaging requirements to determine whether the requested specification is suitable for production.
AOLANSU can provide relevant export and product documents, including Certificate of Analysis (COA), Safety Data Sheet (SDS), product specification sheets, and shipping documentation required for applicable chemical transportation procedures.
AOLANSU combines chemical manufacturing capability, purification technology, analytical testing, hazardous chemical management, and international export experience to support customers with demanding solvent requirements. Instead of evaluating a solvent only by its nominal purity, our quality approach considers the contamination factors that can affect real manufacturing processes.
For semiconductor, electronics, optical, pharmaceutical, and laboratory customers, AOLANSU provides High Purity Isopropyl Alcohol with controlled specifications, traceable batch documentation, flexible packaging, and professional export support. Our goal is to provide a stable material supply that fits the customer's actual process requirements.
If you are sourcing High Purity Isopropyl Alcohol for semiconductor cleaning, precision electronics, optical components, pharmaceutical processing, or laboratory applications, contact AOLANSU with your required purity, impurity limits, packaging, and order quantity.
Shandong Aolansu Environmental Technology Co., Ltd. can provide product specifications, COA information, SDS documentation, packaging options, and international shipping support for qualified B2B customers.
Address
(North of Dongwei Group, West) Houwei Village, Changshan Town, Zouping City, Binzhou, Shandong Province, China
Tel